E-mail: info@plymachine.com WhatsApp:+8619553901259

Views: 0 Author: Site Editor Publish Time: 2026-09-01 Origin: Site

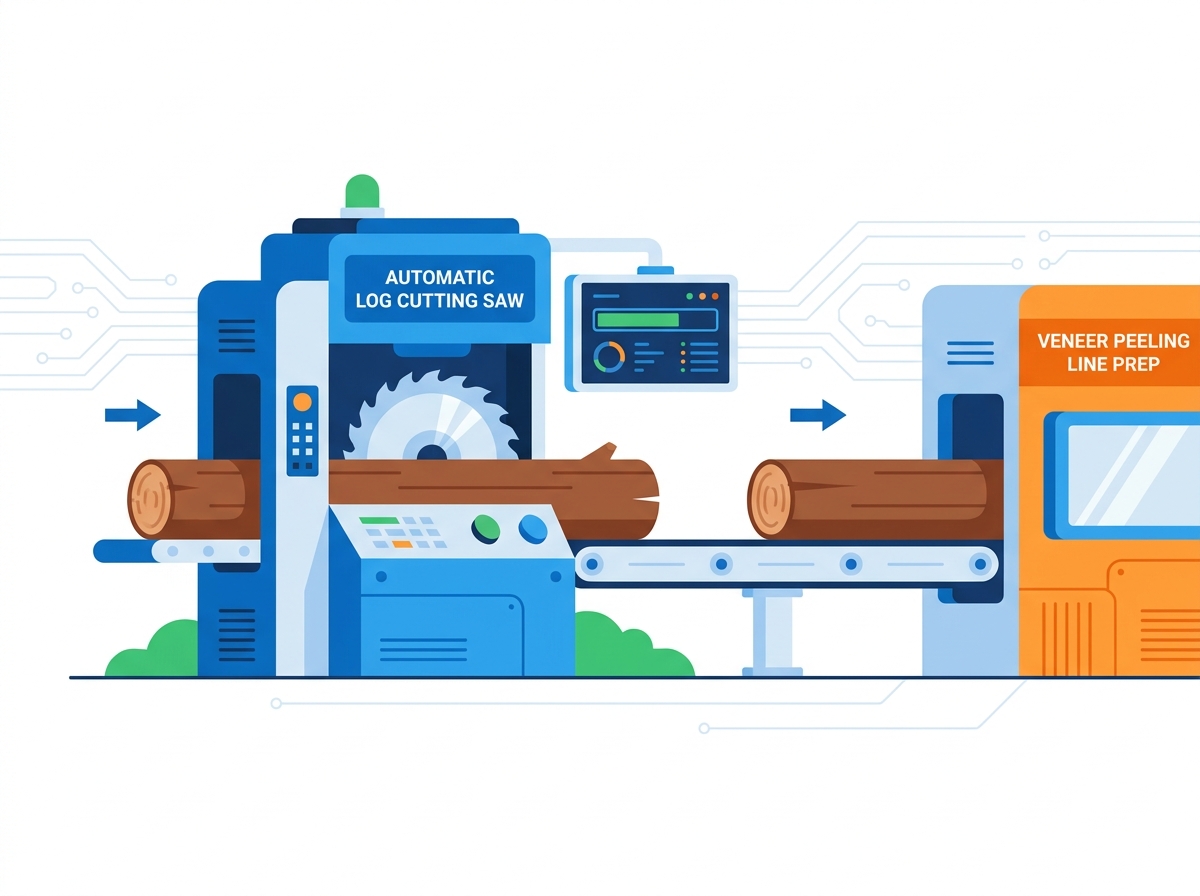
The efficiency of a veneer peeling line is dictated before the log ever reaches the lathe. Imprecise initial cuts directly correlate to reduced veneer yield and increased downstream machine wear. Manual or poorly calibrated log bucking introduces length variances, un-square ends, and throughput bottlenecks. These inconsistencies lead to lathe jams, excessive block waste, and compromised veneer quality. Upgrading to a purpose-built log cutting saw standardizes block preparation. Automated systems maximize usable timber and ensure a continuous material flow to the peeling lathe. This guide breaks down the technical criteria for evaluating and specifying the correct saw for your production facility, focusing on mechanical capabilities, integration requirements, and yield optimization.
Precision Dictates Yield: A log cutting saw must deliver exact, square cuts to prevent spindle chucking failures and minimize rounding waste at the lathe.
Automation Drives Throughput: Transitioning to an automatic log cutting saw eliminates manual measurement errors and matches the high-speed demands of modern veneer peeling lines.
Blade Dynamics Matter: The choice between circular and chain saw configurations fundamentally impacts kerf loss, cycle time, and ongoing maintenance costs.
Integration is Critical: Standalone saws create bottlenecks; optimal ROI requires seamless integration with log decks, centering conveyors, debarkers, and peeling line PLCs.
Lathe performance relies entirely on the geometric accuracy of the incoming block. Un-square log ends cause uneven chuck penetration during the initial clamping phase. When the lathe spindles engage a block with an angled face, one side of the chuck bites deeply into the wood fibers while the opposite side barely makes contact. High-speed peeling generates massive rotational torque. Uneven chucking cannot withstand this torque, leading directly to log spin-outs. A spin-out ruins the block, halts production, and frequently damages the spindle chucks, requiring hours of maintenance to repair.
Precise block length directly influences maximum continuous veneer ribbon recovery. If a block is cut too short, the lathe chucks may fail to engage securely, dropping the block into the trash gate. If cut too long, the block requires excessive rounding. Rounding turns valuable sapwood into low-value fishtails and waste veneer. Exact length control ensures the block matches the knife length perfectly, maximizing the volume of full-sheet veneer recovered from every log processed during a shift.
A high-capacity veneer peeling line consumes blocks rapidly, often processing a block every ten to fifteen seconds. The log cutting station must match or exceed this consumption rate. Cycle time synchronization prevents feedstock starvation at the lathe and eliminates log deck bottlenecks upstream. If the cutting saw cycles too slowly, the peeling line idles, destroying shift productivity and lowering overall plant efficiency.
If the saw cuts faster than the downstream conveyors can clear the blocks, log jams occur at the transfer decks. Proper synchronization requires calculating the average peeling time per block and specifying a saw with a cycle time that maintains a consistent buffer on the centering conveyor. Plant engineers must account for the time it takes to advance the log, clamp it, execute the plunge cut, retract the blade, and kick the block onto the outfeed deck.
High-volume veneer operations must establish strict baseline metrics for acceptable kerf loss and trim waste. Every millimeter of wood turned into sawdust represents lost revenue. Standard bucking practices often result in 10mm to 15mm of kerf loss per cut. Purpose-built veneer saws aim to reduce this kerf to under 8mm while maintaining blade stability under heavy loads.
Measure average kerf loss per cut across a 100-log sample to establish a baseline.
Calculate the volume of lily pads and end-trim waste generated per shift.
Track the frequency of lathe spin-outs directly attributed to un-square block ends.
Monitor the volume of rounding waste generated before a continuous veneer ribbon is achieved.
By utilizing advanced scanning and optimization, facilities can reduce end-trim waste from traditional margins of 50mm down to 20mm. This reduction significantly increases the total volume of peelable wood over an annual production cycle.
Circular saws utilize large-diameter steel blades driven by high-torque electric motors. These systems dominate high-speed veneer operations processing small to medium-diameter timber, typically ranging from 150mm to 600mm in diameter.
Mechanism: A heavy-duty circular blade, often exceeding 1500mm to 2000mm in diameter, mounts to a massive steel arbor. The arbor assembly plunges through the log via hydraulic or electromechanical actuation.
Pros: Circular blades deliver extremely fast cycle times, often completing a cut in under three seconds. They produce highly accurate, perfectly square cuts with a smooth finish on the log ends. The rigid blade resists deflection, making it ideal for continuous, high-speed operations.
Cons: These systems require higher initial capital expenditure due to the massive steel frames required to absorb harmonic vibrations. They are also strictly limited by maximum log diameter due to blade size constraints and arbor interference.
Chain-type saws are the standard for processing oversized timber that exceeds the physical limits of circular blades. Hardwood mills processing old-growth timber rely heavily on these robust systems.
Mechanism: These saws feature heavy-duty harvester chainsaw bars mounted on hydraulic or pneumatic pivot arms. The chain is driven by a high-speed motor, and the bar feeds through the log using controlled hydraulic pressure to prevent stalling.
Pros: Chain saws easily handle massive log diameters, often exceeding 1000mm. They require a lower initial investment and occupy a smaller factory footprint compared to large circular saw enclosures.
Cons: Cutting speeds are significantly slower, taking up to 20 seconds for a large hardwood log. The 3/4-inch pitch chain produces a wider kerf, generating more sawdust waste. The system requires frequent chain sharpening, tensioning, and high volumes of bar oil.
Feature | Circular Log Cutting Saw | Chain-Type Log Cutting Saw |
|---|---|---|
Optimal Log Diameter | Small to Medium (up to 600mm) | Large to Massive (600mm to 1200mm+) |
Cycle Speed | Very Fast (2-5 seconds per cut) | Moderate to Slow (10-30 seconds per cut) |
Cut Finish & Squareness | Excellent / Highly precise | Good / Subject to bar deflection on hard knots |
Kerf Waste | Low (Narrow blade profile, ~8mm) | High (Wider chain gauge, ~15mm) |
Maintenance Focus | Blade retipping, arbor bearing lubrication | Chain sharpening, bar replacement, tensioning |
Manual and semi-automatic systems rely on operator-dependent positioning. The operator visually aligns the log, actuates the clamp, and initiates the cut using manual hydraulic levers. This approach carries a high risk of human error. Operator fatigue leads to inconsistent block lengths, un-square cuts, and reduced daily throughput. Manual systems are entirely inadequate for modern, high-capacity veneer mills.
An automatic log cutting saw transforms the preparation phase. These systems utilize PLC-controlled feeding mechanisms paired with optical or 3D laser scanning. The scanners detect defects, sweep, and taper along the entire length of the stem. The PLC calculates the optimal cut points and automates the clamping and cutting sequence. Automation ensures every block meets strict geometric tolerances without relying on operator judgment, maximizing clear wood recovery.
A saw blade will bind, deflect, or stall if the log moves even slightly during the cut. Effective clamping is non-negotiable. Hydraulic V-clamp systems cradle the log from the bottom and sides, forcing it into a stable, centered position. Overhead hold-downs apply downward pressure to prevent the log from rolling. Evaluating the hydraulic pressure and the surface area of the clamp jaws is critical for heavy timber.
Systems operating at 120 bar to 150 bar provide sufficient holding force for dense hardwoods. The clamp jaws must feature aggressive teeth to bite through loose bark and grip the solid sapwood beneath. Proper stabilization prevents log rotation, ensures a perfectly square end, reduces blade binding, and significantly extends tooling life by preventing lateral stress on the saw arbor.
Modern optimization software dictates yield recovery. 3D laser scanning systems map the entire surface of the log as it moves along the transverse or linear infeed conveyor. The software evaluates the log's sweep (curvature), taper, and visible defects. Instead of cutting fixed lengths blindly, the algorithm calculates optimal bucking solutions in milliseconds.
It determines how to divide the log to yield the highest number of premium blocks while isolating severe defects into waste sections. For example, if a log has a severe sweep in the middle, the software will position a cut directly at the apex of the curve. This strategy minimizes the rounding required at the lathe, maximizing clear wood recovery and ensuring the lathe receives blocks that yield continuous veneer ribbons faster.
The main saw drive must deliver relentless torque. When evaluating drive systems, compare hydraulic motors against direct-drive electric motors. Direct-drive systems utilizing IE3 or IE4 high-efficiency electric motors provide superior energy transfer and lower operational costs. Motor sizing typically ranges from 45kW for smaller softwood lines up to 90kW for heavy hardwood applications.
The drive system must maintain consistent RPM when the blade encounters dense knots, wet sapwood, or frozen timber. A drop in RPM causes the blade to wander, ruining the squareness of the cut and generating excessive heat. Proper motor sizing determines the saw's ability to power through difficult wood species without stalling or tripping thermal overloads in the electrical cabinet.
Veneer mills frequently process multiple wood species. The cutting saw must adapt to varying densities and specific gravities. Hardwoods like birch and oak require slower feed speeds and specific blade pitch configurations to prevent burning the wood and warping the blade. Softwoods like pine and fir allow for faster feed speeds but generate stringy sawdust that can clog extraction systems.
Adjust the Variable Frequency Drive (VFD) on the saw feed mechanism to match the plunge rate to the timber density.
Select the correct tooth geometry; use fewer teeth with deeper gullets for softwoods to clear chips rapidly.
Increase the flow of blade coolant or lubrication when processing highly resinous species like pine to prevent pitch buildup.
Selecting the correct tooling and feed rate prevents motor stalling and ensures a clean cut across different timber densities, maintaining high throughput regardless of the raw material supply.
High-speed cutting generates massive volumes of sawdust and heavy offcuts. Inadequate waste management leads to mechanical fouling and severe fire hazards. The saw enclosure must feature integrated extraction hoods connected to a high-CFM dust collection system. The extraction system must pull enough vacuum to clear wet, heavy sawdust before it packs into the machine frame.
Automated drop-out gates located directly below the cutting zone allow heavy offcuts, lily pads, and shattered log ends to fall directly onto a vibrating waste conveyor. Efficient waste removal maintains continuous operation, prevents sawdust from packing into the arbor bearings, and eliminates the need for manual clearing during production shifts. A clean machine runs cooler and experiences fewer sensor faults.
A high-performance saw requires robust material handling to function effectively. Step-feeders singulate logs from the bulk deck, presenting them one at a time to the saw infeed. Heavy-duty log kickers eject the cut blocks onto the outfeed deck. Centering conveyors then transport the blocks directly to the peeling lathe. These handling systems must operate without manual intervention.
The speed of the conveyors must synchronize with the saw's cycle time and the lathe's consumption rate to maintain a seamless, continuous flow of material. If the step-feeder cycles at 12 logs per minute, the saw must complete its clamping, cutting, and retracting sequence in under five seconds to prevent a backlog. Variable speed drives on all transfer decks allow operators to fine-tune the flow of blocks.
The placement of the cutting saw relative to the debarker impacts blade life and block quality. Pre-cut debarking involves running the long log through a ring debarker before it reaches the saw. This sequence removes rocks, mud, and abrasive grit from the bark. Cutting clean wood significantly extends blade life and reduces sharpening frequency.
Handling debarked logs requires specialized conveyors with non-marring surfaces to prevent damage to the exposed sapwood. Post-cut debarking involves cutting logs with the bark still on, then sending the short blocks through a rosserhead debarker. This sequence protects the wood during transport but subjects the saw blade to severe abrasion, requiring frequent tooling changes and increasing consumable costs.
Isolated machinery limits plant efficiency. The saw's Programmable Logic Controller (PLC) must communicate directly with central plant control systems. Evaluating communication protocols like Profinet or EtherNet/IP ensures the saw integrates seamlessly with the log deck and the peeling lathe. This network compatibility allows for automated speed adjustments based on downstream bottlenecks.
Integrated data analytics track shift yield, downtime events, and Overall Equipment Effectiveness (OEE). Access to real-time OEE reporting enables plant managers to identify inefficiencies and optimize the bucking process continuously. If the saw experiences repeated micro-stops due to sensor faults, the OEE dashboard highlights the exact component causing the delay, allowing maintenance to resolve the issue before it impacts the shift quota.
Log cutting involves massive moving parts, high-speed blades, and heavy timber. Strict adherence to safety standards is mandatory. The saw station must include heavy-duty steel safety enclosures to contain flying debris, shattered knots, or broken carbide teeth. Acoustic dampening cabins are necessary to reduce noise exposure to acceptable OSHA or CE levels, often bringing the ambient noise down from 110 dB to under 85 dB.
Light curtains and safety interlocks must guard all access points, instantly halting the machine if an operator breaches the safety zone. Emergency stop integrations must tie into the broader line control, ensuring a stop command at the lathe also halts the saw infeed, preventing blocks from piling up on the transfer decks during an emergency event.
Evaluating a new saw requires balancing upfront investment against long-term operational savings. Automated systems demand a higher initial CapEx but drastically reduce OpEx by minimizing labor requirements and eliminating manual measurement errors. Reallocating operators from manual bucking stations to quality control roles improves overall plant efficiency.
The primary financial driver is increased veneer yield. Consumable costs also play a major role in OpEx. Circular blades require periodic retipping and tensioning, whereas chain systems demand frequent chain replacement, bar resurfacing, and high volumes of bar oil. Analyzing these ongoing consumable costs against the expected cycle speed determines the true operational value of the equipment over a ten-year lifespan.
Tooling maintenance dictates machine uptime. A dull blade ruins cut quality, increases motor strain, and slows production. Facilities must assess the hidden costs of blade maintenance. Investing in an in-house sharpening room provides immediate control over tooling quality and reduces inventory requirements. It requires purchasing CNC profile grinders and training specialized technicians.
Maintenance Task | Frequency | Impact on Production |
|---|---|---|
Visual Blade Inspection | Every Shift | Prevents catastrophic blade failure and identifies chipped teeth early. |
Arbor Bearing Lubrication | Weekly | Maintains smooth rotation and prevents heat buildup in the drive assembly. |
Hydraulic Filter Replacement | Every 500 Hours | Ensures consistent clamping pressure and prevents valve sticking. |
Scanner Calibration | Monthly | Maintains length accuracy and optimizes yield recovery algorithms. |
Relying on external tooling vendors eliminates the need for specialized sharpening equipment but requires a larger inventory of spare blades to cover transit times. The chosen infrastructure must guarantee that a sharp, properly tensioned blade is always available to prevent unexpected downtime.
The justification for upgrading to an optimized cutting system relies on yield improvement. A framework for calculating ROI focuses on the percentage increase in usable block volume. By utilizing 3D scanning and precise PLC controls, a mill can reduce trim waste and kerf loss.
A mere 1% to 3% increase in usable block volume translates to a massive reduction in raw material costs over a year. Optimized cutting accuracy ensures fewer spin-outs at the lathe and less rounding waste. This precision directly converts previously wasted wood into high-value veneer sheets, accelerating the payback period for the new equipment.
Replacing a core piece of machinery risks prolonged installation downtime, which halts the entire peeling line. Extended downtime devastates monthly production quotas. To mitigate this risk, require modular pre-assembly from the equipment manufacturer. The machine should arrive on site in large, pre-wired modules rather than individual components.
Mandate a comprehensive Factory Acceptance Testing (FAT) phase prior to delivery. During the FAT, the saw must process sample logs to verify cycle times, cutting accuracy, and software integration. Identifying and resolving mechanical or programming issues at the factory ensures a rapid, plug-and-play installation on the mill floor, minimizing the disruption to ongoing operations.
Complex automated systems can overwhelm maintenance staff accustomed to older, mechanical equipment. If operators do not understand the optimization software, they will bypass it, negating the yield benefits and reverting to manual cutting modes. Mitigation requires comprehensive vendor training programs covering both operation and troubleshooting.
The Human-Machine Interface (HMI) must feature clear, intuitive graphics and diagnostic screens that pinpoint sensor faults immediately. Secure a Service Level Agreement (SLA) for spare parts availability to ensure critical components like laser scanners, proportional hydraulic valves, and PLC modules are readily accessible, preventing minor failures from causing days of downtime.
Environmental factors severely impact cutting performance. Processing frozen logs during winter months increases wood hardness, leading to premature blade dulling and motor stalling. High-grit bark from logs dragged through mud acts like sandpaper on cutting tools, destroying carbide teeth in hours.
To mitigate these variables, specify heavy-duty stellite-tipped blades designed specifically for frozen timber. Integrate a log debarker prior to the cutting station to remove abrasive grit. Ensure all electrical cabinets and hydraulic reservoirs are climate-controlled with internal heaters to maintain fluid viscosity (e.g., using ISO 32 hydraulic oil in winter) and protect sensitive electronics during freezing temperatures.
Conduct a time-study on your current log bucking process to quantify existing trim waste, kerf loss, and lathe spin-out rates.
Request customized throughput simulations and tooling cost estimates from shortlisted equipment vendors based on your specific log diameters and wood species.
Evaluate your internal tooling maintenance capabilities to determine whether an in-house sharpening room or a vendor-managed inventory system fits your operational model.
Schedule a Factory Acceptance Test (FAT) with your chosen manufacturer to verify cycle times and software integration before taking delivery of the equipment.
A: Veneer-specific saws prioritize absolute squareness and precise length measurement to ensure the log mounts perfectly in the peeling lathe chucks. Standard bucking saws prioritize rough volume and rapid processing, often leaving angled ends that cause lathe spin-outs.
A: By utilizing 3D laser scanning and PLC controls, the system calculates exact cut points to eliminate human measurement error. This optimization reduces trim waste, minimizes kerf loss, and maximizes the length of the peelable block sent to the lathe.
A: Circular saws are faster and provide a cleaner, squarer cut, making them ideal for high-speed lines processing small to medium logs. Chain saws are necessary for very large diameter logs but operate with slower cycle times and generate wider kerf waste.
A: If a log shifts or rotates during the cut, the blade will bind, stall the motor, or deflect. Secure hydraulic clamping ensures a perfectly square cut, prevents mechanical damage to the saw arbor, and extends blade life.
A: Frozen wood is significantly harder, which increases motor strain and accelerates blade dulling. Processing frozen logs requires specialized stellite-tipped blades, slower feed speeds, and climate-controlled hydraulic systems to maintain fluid viscosity.
A: Debarking before cutting removes rocks and abrasive grit, which significantly extends saw blade life. However, it requires specialized conveyors to prevent damaging the exposed wood. Post-cut debarking protects the wood during transport but increases blade wear.