E-mail: info@plymachine.com WhatsApp:+8619553901259

Views: 0 Author: Site Editor Publish Time: 2026-08-13 Origin: Site

Outsourcing blade sharpening causes unacceptable downtime in modern woodworking operations. Dull blades constantly reduce your yield, increase machine wear, and spike energy consumption. When production stops to wait for fresh blades, profitability takes an immediate hit.
You can eliminate these logistical headaches easily. Investing in an in-house industrial knife grinder recovers your control over maintenance cycles and operational expenditure (OPEX). It transforms a vulnerable supply chain step into a predictable internal process.
This guide provides a comprehensive technical evaluation framework. We will help you shortlist industrial knife grinding equipment specifically for heavy-duty forestry and woodworking applications. You will learn how to match machine specifications to your precise blade requirements and production volume.
Tolerance drives the investment: Veneer peeling requires micro-precision to prevent wood tearing, while chipper blades prioritize aggressive edge durability.
Coolant systems are non-negotiable: Effective heat dissipation is mandatory to prevent metallurgical damage and edge burning during heavy grinding passes.
Automation yields consistency: CNC or PLC-controlled grinders reduce operator error and labor costs compared to manual sharpening methods.
Size and scalability matter: Machine bed length and clamping mechanisms must accommodate your longest blades and future operational expansions.
Bringing blade maintenance in-house represents a significant shift in operational strategy. You must weigh the initial capital expenditure (CAPEX) against long-term efficiency gains. Facilities often discover the return on investment materializes much faster than anticipated.
Compare the cumulative costs of third-party sharpening services against purchasing your own equipment. External vendors charge per inch of blade. They also pass along rising shipping and handling fees. Over several years, these continuous external expenses easily surpass the CAPEX of dedicated grinding machinery. Controlling the process internally locks in your OPEX and insulates you from vendor price hikes.
Logistical delays ruin production schedules. Shipping blades back and forth across the country adds days or weeks of lead time. By controlling the sharpening schedule, you eliminate these unpredictable shipping delays. You minimize equipment idle time completely. If a foreign object damages a blade mid-shift, you can regrind it immediately and resume production within hours.
In-house grinding grants you total authority over blade geometry. You can customize edge angles and bevels to match specific operational variables.
Adjust angles for different wood species and densities.
Modify bevels to handle seasonal moisture changes.
Fine-tune the edge finish to meet exact daily production requirements.
External vendors apply standard factory grinds. They rarely tailor their work to your specific daily environmental conditions.
We must acknowledge a practical reality here. Low-volume operations may not justify a heavy machinery CAPEX right away. In-house grinding demands a real commitment. You must dedicate resources to thorough operator training and strict machine maintenance. If you only change blades once a month, external services might remain the logical choice.
Woodworking blades look similar from a distance. However, their industrial applications demand entirely different grinding approaches. Understanding these metallurgical and geometric differences prevents costly purchasing mistakes.
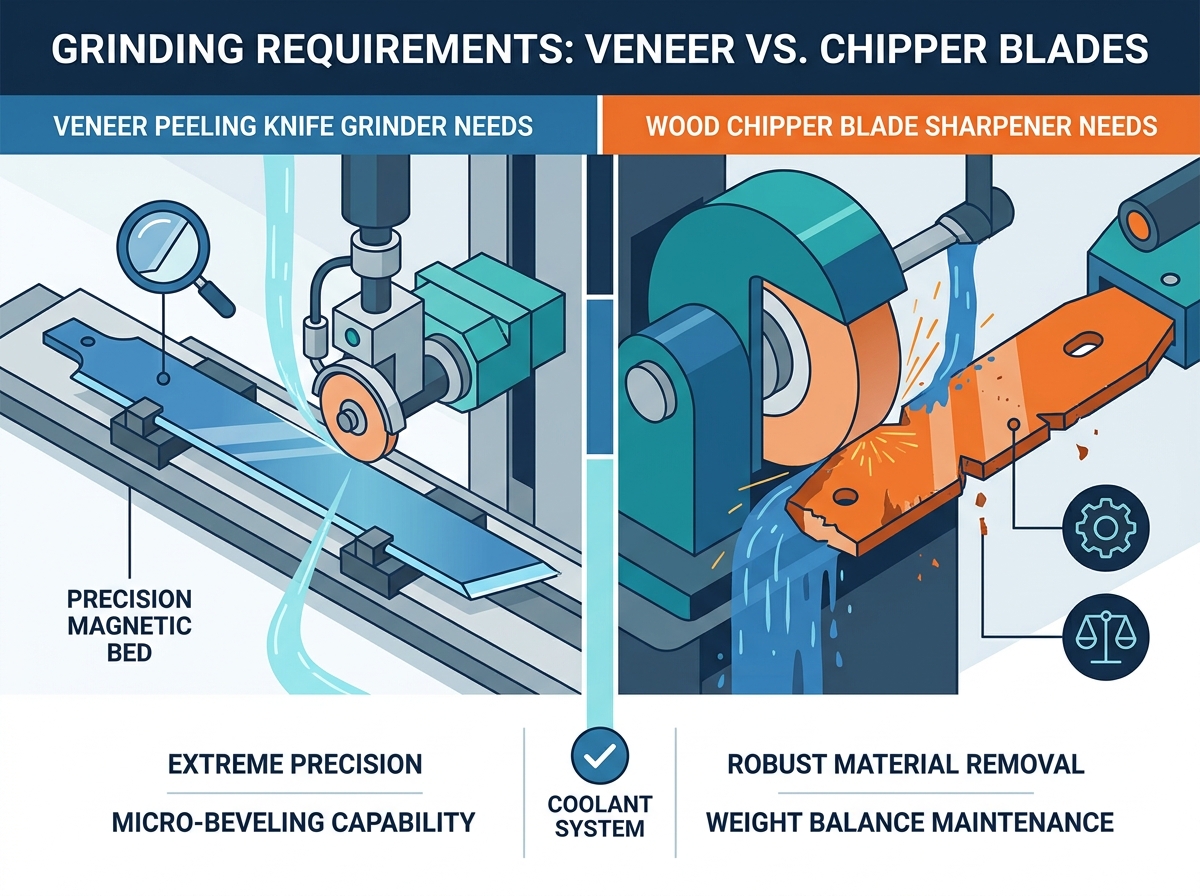
Veneer production requires extreme precision. A veneer peeling knife grinder must operate with zero deflection. Any vibration translates directly into blade chatter. This chatter causes wood tearing and ruins high-value continuous veneer sheets.
These blades also necessitate precise micro-beveling capabilities. A micro-bevel strengthens the cutting edge while maintaining razor-like sharpness. Grinding equipment for this application needs ultra-fine finishing wheels. The surface finish must be practically mirror-like to slice cleanly through wet logs without creating friction marks.
Forestry chippers live a brutal life. They constantly encounter dirt, frozen wood, and hidden rocks. Therefore, a wood chipper blade sharpener focuses heavily on robust material removal. The machine must rapidly grind away deep nicks, large chips, and heavy wear zones.
Furthermore, maintaining exact weight balance across chipper blade sets is critical. Rotors spin at extremely high RPMs. If one blade weighs slightly less than its counterpart, the imbalance causes catastrophic rotor vibration. This vibration destroys main bearings rapidly. Your grinding process must ensure identical material removal across every blade in a specific set.
Veneer Peeling vs. Chipper Blade Requirements
Feature Focus | Veneer Peeling Knives | Wood Chipper Blades |
|---|---|---|
Primary Goal | Flawless, tear-free wood slicing | Aggressive impact reduction |
Precision Need | Micro-tolerances, zero deflection | Consistent geometry, exact weight matching |
Material Removal | Light, ultra-fine finishing passes | Heavy, rapid bulk steel removal |
Edge Geometry | Complex micro-bevels required | Standard straight bevels (30°-37°) |
Selecting the right machine architecture determines your daily workflow efficiency. Manufacturers primarily build these machines in two structural formats. You must align the machine type with your specific blade inventory.
The linear grinder dominates heavy industry. The mechanism operates simply but robustly. The blade remains completely stationary on a heavy magnetic bed. The grinding head itself moves back and forth along a precision track.
This configuration works best for extremely long veneer knives. It also handles heavy chipper blades requiring high stability and precision. Moving the head rather than the heavy blade eliminates inertia problems. It guarantees uniform straightness across blades exceeding two meters in length.
Rotary grinders utilize a different physical approach. Blades are mounted securely on a large rotating circular table. This table spins continuously, passing the blades underneath a stationary grinding head.
Rotary models excel at high-volume batch sharpening. They handle shorter blades exceptionally well. You can load dozens of small inserts or planer blades simultaneously. The continuous circular motion provides aggressive material removal rates.
Machine control systems range from fully manual hand-wheels to advanced digital automation. Manual feeding remains highly labor-intensive. Operators must stand at the machine, adjusting the downfeed for every single pass. This introduces human error and fatigue.
Automated downfeed systems use Programmable Logic Controllers (PLC) or Computer Numerical Control (CNC). They offer set-and-forget consistency. You program the total removal amount and the spark-out passes. The machine handles the rest autonomously. Automation delivers excellent ROI through drastically reduced scrap rates. It also lowers dedicated labor hours, freeing your personnel for other tasks.
Evaluating industrial equipment requires looking past the marketing brochures. You must scrutinize five mechanical subsystems. These components dictate the lifespan and accuracy of your investment.
How the machine holds the blade determines the final edge straightness. Mechanical clamps often pinch the steel unevenly. This pinching causes microscopic blade distortion. Once unclamped, the blade bows back to its natural shape, ruining the straight edge.
Assess electromagnetic chucks instead. They provide uniform holding power across the entire blade surface. High-end magnetic beds feature variable holding power. This prevents thin veneer knives from warping during the grinding process.
Heat is the absolute enemy of hardened steel. Insufficient cooling damages the metallurgical structure instantly. Evaluate flood coolant systems for high volume flow rates. A steady deluge of liquid must hit the exact point of contact.
Filtration matters equally. Magnetic separation units extract microscopic metal swarf from the returning fluid. Clean coolant keeps the grinding wheel pores open. A clogged wheel causes rapid heat buildup and edge burning.
Your blade material dictates your abrasive requirements. High-Speed Steel (HSS) requires different wheels than carbide-tipped knives. Check the machine's compatibility with different abrasives.
Aluminum Oxide: Excellent for general-purpose carbon steel.
CBN (Cubic Boron Nitride): Ideal for hard HSS blades.
Diamond: Mandatory for sharpening brittle carbide edges.
Ensure the machine accepts common wheel diameters. Proprietary wheel sizes limit your consumable supply chain options.
Look for incredibly heavy cast-iron machine bases. Cast iron absorbs high-frequency vibrations significantly better than welded steel plates. Rigidity prevents chatter marks on the finished blade.
Check the spindle motor horsepower. The motor needs sufficient torque to maintain a constant wheel RPM under heavy downfeed loads. If the motor bogs down during a heavy pass, the wheel will glaze and burn the blade.
Never buy a machine based only on your current maximum blade length. Ensure the machine handles your longest blade easily, but add a 15-20% margin. Future equipment upgrades often utilize longer knives. Sizing up your stroke length capacity now prevents forced machine replacements later.
Purchasing the equipment represents only the first step. Successful integration requires thorough facility preparation. Do not overlook the physical and safety demands of heavy grinding machinery.
Industrial grinders command significant floor space. Detail the exact footprint requirements before ordering. The traveling head requires clearance extending past the main machine body.
Verify your heavy-duty electrical drops. These machines demand stable 3-phase power. Check your floor load-bearing limits as well. A large cast-iron grinder filled with coolant weighs several tons. It requires a reinforced, perfectly level concrete pad to maintain grinding geometry.
Grinding large, razor-sharp blades presents severe workplace hazards. You must mandate strict safety protocols. Provide proper rigging and lifting tools, like magnetic hoists, to handle heavy blades.
Enforce strict adherence to lock-out/tag-out (LOTO) procedures during wheel changes and cleanings. Operators need comprehensive training on wheel dressing, feed rates, and emergency shutdown protocols.
Your OPEX budget must factor in ongoing consumable costs. Implement robust inventory management for essential supplies. You will consume grinding wheels, synthetic coolants, rust inhibitors, and truing tools regularly. Running out of a specific CBN wheel halts your sharpening operation entirely.
A grinding environment generates highly abrasive slurry. This mixture of metal dust and grit destroys precision moving parts quickly. Address the necessity of daily machine clean-downs. Operators must wash down the magnetic bed and clear the coolant channels.
If abrasive slurry penetrates the way-covers, it will destroy the linear bearings and guide rails. Implement a strict preventative maintenance schedule. Grease the fittings and check the coolant pH levels weekly to prevent internal rust.
Bringing blade sharpening in-house transforms a frustrating maintenance bottleneck into a streamlined operational advantage. You must meticulously match the machine's rigidity, cooling capacity, and automation level to your specific blade type. Heavy material removal requires raw horsepower, while micro-beveling demands vibration-free precision.
Take proactive next steps before contacting vendors. Gather your exact blade dimensions and weights. Calculate your current monthly sharpening expenditures, including shipping costs. Define your acceptable tolerance metrics. Armed with this data, you can confidently engage equipment manufacturers for accurate quotes and realistic test grinds.
A: Maintenance cycles depend heavily on operating hours and wood cleanliness. Clean timber might allow 40 to 60 hours of operation between sharpenings. Processing dirty, frozen, or rock-filled wood can degrade chip quality in just a few hours. Monitor your output closely; when chips become stringy or production slows, sharpen immediately.
A: Yes, high-end linear grinders handle both successfully. However, the machine must feature precise variable angle adjustments. Operators must also perform appropriate wheel changes between batches. Remember that while one machine can do both, achieving the micro-tolerances required for veneer takes significantly more setup time.
A: Most industrial chipper blades utilize a grinding angle between 30° and 37°. A steeper angle cuts aggressively but dulls faster. A wider angle increases impact resistance. Always consult your original equipment manufacturer specs to determine the exact optimal geometry for your specific chipper model.
A: Preventing edge burn requires a strict combination of variables. Use the proper wheel grit for your steel type to prevent clogging. Utilize very slow, consistent feed rates during material removal. Most importantly, flood the cutting zone with high-volume, properly mixed synthetic coolant to dissipate heat instantly.