E-mail: info@plymachine.com WhatsApp:+8619553901259

Views: 0 Author: Site Editor Publish Time: 2026-08-24 Origin: Site

Plywood manufacturing often hits a critical bottleneck early in the cycle. Inconsistent log preparation slows down the entire factory floor. You cannot produce high-quality panels when unprocessed timber piles up. Inefficient peeling halts downstream operations entirely.
Traditionally, factories relied heavily on manual bark removal to prepare timber. However, rising labor costs and strict quality demands force an industry shift. Factory floors need reliable, fast, and safe methods. Automated processing addresses these modern operational challenges directly.
This article provides factory managers and decision-makers with a detailed, objective comparison. We will explore the operational and financial differences between manual stripping methods and machinery upgrades. You will learn how modernizing this step directly impacts downstream yield and profitability.
Transitioning to a hydraulic log debarker shifts costs from unpredictable manual labor to predictable operational maintenance (Capex vs. Opex).
Automated debarking directly extends the lifespan of cutting knives on the veneer peeling line by consistently removing embedded dirt and debris.
Manual removal often results in higher usable wood loss and uneven log surfaces, negatively impacting downstream plywood yield.
Implementation of hydraulic systems requires upfront footprint planning, operator safety training, and routine fluid/pressure maintenance.
Debarking represents a critical pass-or-fail stage before timber ever enters the factory floor. The cambium layer and outer bark protect trees in the wild. In a factory setting, they become major obstacles. Bark absorbs moisture unevenly. It also hides severe defects. Factory managers must view bark removal as the first true quality control checkpoint. If you fail here, every subsequent process suffers.
Bark naturally retains sand, rocks, and environmental grit from the logging site. Dragging logs through dirt compounds this problem. Poor debarking pushes this abrasive material directly into your cutting machinery. This grit acts like sandpaper against precision steel. The direct consequence is accelerated wear and tear on the veneer peeling line. Factory operators must halt production to replace damaged knives. Unplanned downtime destroys daily production quotas. It inflates maintenance budgets rapidly.
Successful debarking follows strict success criteria. A factory must achieve maximum bark removal across the entire log surface. Operators must ensure minimal damage to the usable sapwood underneath. Finally, the preparation stage must deliver consistent throughput. The debarking speed must seamlessly match your lathe peeling capacity. You achieve optimal economics only when logs flow without interruption.
Many legacy facilities still rely on the standard manual baseline approach. Workers use drawknives, chainsaws, or manual spuds to strip logs. Crews manually rotate massive timber blocks. They strike the bark repeatedly until the white wood shows. This method requires minimal upfront equipment investment. However, it introduces massive hidden operational burdens.
Manual labor imposes severe physical tolls on workers. The repetitive swinging and pulling motions cause joint stress. Factories experience extremely high turnover rates in debarking crews. You constantly hire and train new personnel. Furthermore, manual crews face strict scalability limits. You cannot quickly scale production to meet sudden demand spikes. Adding more workers requires more space, which is rarely available safely.
Safety hazards represent a massive compliance risk. Manual log handling involves heavy, unpredictable rolling timber. Workers use sharp, high-velocity hand tools in close proximity to each other. Slips, trips, and lacerations happen frequently. These incidents trigger expensive workers' compensation liabilities. Factories also face regulatory fines for compliance failures. Insurance premiums rise when safety records drop.
Hidden wood loss further cripples your profitability. Manual fatigue inevitably leads to inconsistent quality. A tired worker leaves stubborn bark patches behind. This remaining debris damages downstream machinery. Conversely, an aggressive worker chops too deeply into the log. They remove valuable sapwood alongside the bark. Every inch of lost wood directly reduces your final plywood yield. This variable quality destroys predictable profit margins.
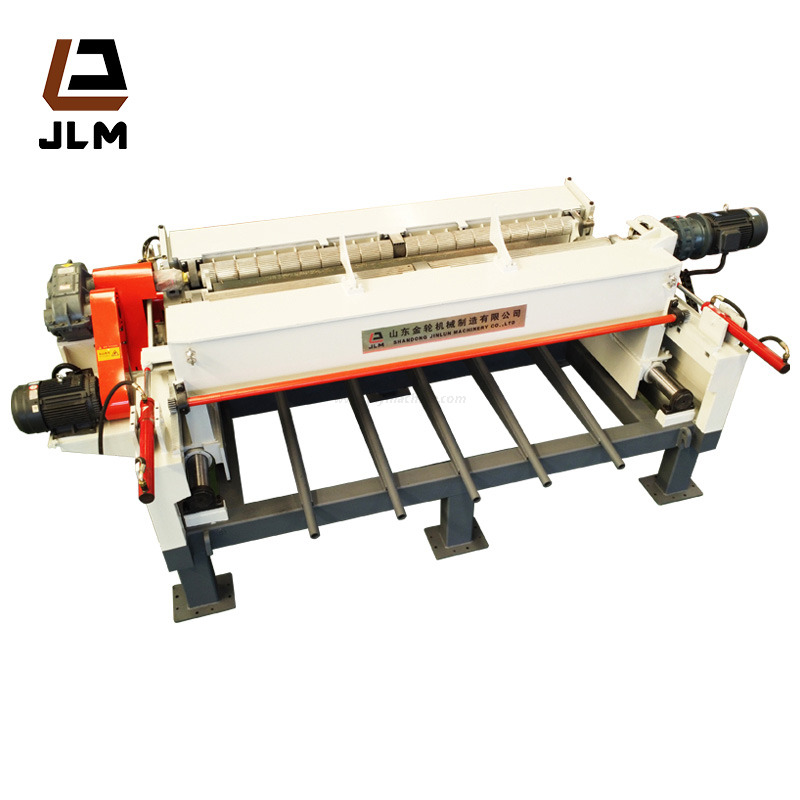
A modern hydraulic log debarker is heavy-duty automated machinery designed to strip timber efficiently. It functions entirely differently from mechanical friction drum debarkers. Drum systems tumble multiple logs together, using friction to rub the bark away. The hydraulic alternative processes logs individually. It uses powered cutting heads and rotating mechanisms to shave the surface clean.
The core mechanisms rely on intense hydraulic pressure. The machine uses fluid power to drive peeling rollers and feed mechanisms. Sensors detect the log diameter dynamically. The hydraulic system maintains consistent contact against the wood. It adapts instantly to irregular, curved, or frozen logs. Mechanical springs often fail to provide this necessary adaptability. Fluid pressure ensures the cutting teeth glide smoothly over contours without jamming.
Integration into the production line is seamless. A standard log debarker sits directly upstream from the processing center. Conveyor belts carry raw timber into the machine. The equipment strips the log in seconds. It then ejects the processed, uniform timber straight into the veneer lathe. This creates a continuous, unbroken production loop. The machinery eliminates chaotic staging areas. It transforms a batch process into a smooth, flowing operation.
Speed determines factory revenue. A dedicated manual crew might process 50 to 80 logs per shift. Their output drops significantly during extreme weather or late afternoon hours. Human endurance dictates the maximum daily output.
A standard hydraulic debarker processes hundreds of logs per hour. It operates at a constant velocity regardless of the time of day. Hydraulic systems entirely eliminate the "waiting on logs" bottleneck. Your veneer stage machinery runs continuously. This speed parity ensures your most expensive cutting assets never sit idle. The return on investment accelerates when your lathe runs at full capacity.
Precision matters just as much as speed. Hydraulic sensors dictate exactly how deep the cutting teeth engage. Adjustable pressure controls prevent aggressive gouging. The machine shaves the bark while leaving the valuable structural fiber intact. Manual work, especially when rushed, routinely damages the cambium layer. Human error directly shrinks the usable diameter of the log.
Waste management also improves drastically. Manual removal scatters debris across the yard. Workers must pause stripping to sweep and shovel bark into bins. Hydraulic machines centralize bark waste automatically. Conveyor belts catch the stripped bark beneath the rollers. They route the debris into hoppers for easy disposal. Many factories repurpose this clean, localized waste as biomass fuel. They heat their drying kilns using their own manufacturing byproducts.
Manual labor relies on ongoing variable costs. You pay hourly wages, overtime, healthcare benefits, and injury costs. These expenses climb annually due to inflation and labor shortages. They offer zero return on investment. You simply pay to maintain the status quo.
Automated systems shift the burden to fixed capital expenditure (Capex) and predictable operating expenses (Opex). You purchase the machine once. Ongoing costs become highly predictable. You budget for hydraulic fluids, grease, and periodic roller replacements. To calculate the break-even point, you must compare these two structures directly.
Calculate your break-even point by comparing your current monthly manual debarking expenses against the monthly financed cost of the machine plus maintenance. Factor in the value of increased plywood yield. Most high-volume factories reach a break-even point within 14 to 24 months. After that period, the labor savings convert directly into net profit.
The chart below highlights the primary operational differences between the two methods.
Processing Efficiency and Output Comparison
Feature | Manual Bark Removal | Hydraulic Automated System |
|---|---|---|
Processing Speed | 50-80 logs per shift | 200+ logs per hour |
Wood Yield Damage | High (gouging and fatigue errors) | Low (sensor-guided precision) |
Safety Hazards | High (lacerations, crushing, joint stress) | Low (enclosed operation) |
Waste Handling | Scattered, requires manual cleanup | Centralized via conveyors |
Scalability | Poor (requires more hiring/space) | Excellent (adjustable feed rates) |
Upgrading to heavy machinery is not instant. Proper planning ensures a smooth transition.
Footprint & Layout
You must address spatial requirements early. Hydraulic machines require substantial physical footprints. You cannot simply drop the machine into an old work zone. You must plan for robust infeed and outfeed conveyors. The factory floor must accommodate the swing radius of loading machinery. You need clear paths for maintenance access and debris removal. Proper layout prevents new bottlenecks from forming around the automated system.
Maintenance Requirements
Owning hydraulic equipment demands strict discipline. Be transparent about the reality of industrial maintenance. Neglect destroys hydraulic pumps quickly. Factories must implement rigorous preventive routines.
Operators must conduct daily visual inspections for leaks.
Maintenance teams must perform weekly hydraulic hose checks.
Technicians must monitor fluid viscosity carefully during cold-weather operations.
Workers must clear debris jams from the roller mechanisms continuously.
Operator Training
Replacing manual labor does not mean achieving zero labor. It means upskilling your existing workforce. You elevate workers from manual laborers to machine operators. They must learn to safely monitor control panels. They need to understand pressure gauges and emergency stop protocols. Proper training empowers them to perform routine preventive maintenance. Well-trained operators prevent catastrophic machine failures. They ensure the equipment delivers its promised return on investment.
Here is a recommended rollout sequence for factory managers:
Audit your current factory floor space to measure conveyor clearances.
Assess your power grid capacity to handle heavy hydraulic pump loads.
Select one supervisor to become the dedicated hydraulic maintenance specialist.
Run the automated machine in parallel with the manual crew for one week to build buffer stock.
Fully transition logs to the automated line once operators prove competent.
Manual debarking avoids large upfront capital expenditures. However, it acts as a permanent ceiling on a factory's production capacity and profitability. Relying on human muscle guarantees inconsistent quality. It accelerates the degradation of downstream peeling knives. It ultimately wastes valuable wood fiber.
Moving toward hydraulic machinery unlocks true manufacturing scale. It stabilizes your daily output. It protects your downstream equipment from abrasive dirt. The transition replaces chaotic manual labor with predictable, systematic efficiency.
Take immediate action to evaluate your current setup. Audit your current log processing bottleneck this week. Calculate your exact monthly knife-replacement costs on the peeling line. Finally, request throughput specifications from equipment manufacturers based on your specific regional wood species.
A: Yes. Modern systems feature adjustable hydraulic pressure settings. Operators increase the PSI for dense hardwoods to ensure the teeth bite through tough bark. They reduce the pressure for softer woods like pine. This adjustability prevents crushing the sapwood while maintaining high processing speeds.
A: Automated machines create a perfectly cylindrical, clean log. They remove abrasive grit that otherwise dulls cutting knives. Sharp knives cutting a uniform surface produce smooth, continuous veneer sheets. This reduces panel weak points, limits patching requirements, and ultimately yields a higher-grade plywood product.
A: Maintenance follows a strict schedule to prevent downtime. Operators perform daily greasing of moving parts and clear debris from the rollers. Technicians conduct weekly hydraulic fluid level and hose integrity checks. Seasonal inspections focus on replacing worn cutting teeth and assessing pump health.
A: Yes, but within specific mechanical limits. Hydraulic feed rollers pivot and adjust dynamically to handle moderate log taper and sweep. Heavy hydraulic pressure forces the cutting heads over surface knots. However, extreme crooks or massive burls may still require manual chainsaw trimming before feeding.